Mr Kidman's Classroom


Revise the key ideas
Sources and properties
- Extraction and refining — Metal ores are mined, processed and refined into usable metals; the extraction route depends on reactivity. Steelmaking refines iron and controls carbon/alloying elements. Aluminium extraction is energy-intensive, making recovery of clean scrap valuable. Mining and processing can affect habitats, water and communities.
- Ferrous selection — Mild steel suits tough brackets and frames and is relatively easy to form. High-carbon steel can provide hard cutting edges after suitable heat treatment. Cast iron suits some cast rigid parts but is brittle; stainless steel uses alloying for corrosion resistance and can suit utensils.
- Non-ferrous selection — Aluminium is low-density and has a protective oxide layer; copper conducts heat and electricity well. Brass is a copper–zinc alloy; bronze is commonly copper–tin. Zinc can protect steel by galvanising. Costs, joining and galvanic interactions matter alongside mass or conductivity.
When different metals are in electrical contact in a suitable wet environment, one can corrode faster. This is a galvanic interaction, so the combination matters as well as each metal on its own.
- Tin and tool alloys — Tin is a soft non-ferrous metal used in coatings and alloys; a coating on steel must remain suitable for the intended environment. High-speed steel contains alloying elements that help cutting tools retain hardness at elevated working temperatures. Compare its wear/heat properties with plain low-carbon steel for a tool edge.
- Heat treatment — Annealing softens suitable metals and can improve working after deformation; the heating and cooling procedure depends on the alloy. Hardening and tempering can tailor suitable steels for cutting tools. Do not use one universal cooling rule for all metals.
Hardening suitable steel increases hardness; tempering after hardening reduces brittleness and adjusts the balance of properties. The correct treatment depends on the steel and must be taught with the appropriate equipment.
- Utensils and tools — A cooking utensil needs appropriate heat transfer, corrosion resistance, cleanability and food-contact safety. A hand tool may need a hard wear-resistant edge plus a tough body or handle. Select and justify each part rather than claiming one metal is ideal for every tool.
Stock and forming
- Stock forms — Metals come as sheet, plate, rod, bar and tube with standard dimensions. Tube can give useful bending stiffness at lower mass than a solid section. Standard rivets, machine screws, nuts and bolts need correct diameter, thread and load capacity. Include cutting and machining allowances.
- Cutting and drilling — Sawing and shearing remove or separate material using appropriate tooling; burrs must be removed. Drilling requires secure workholding, correct tool/feed and suitable lubrication where specified. A depth stop limits travel but does not check every feature or prevent every hazard.
Burrs are sharp raised edges or fragments left by cutting or drilling. Feed concerns how quickly the tool and work advance relative to each other; the correct settings come from the taught procedure.
- Turning and milling — Turning rotates work against a tool, usually for cylindrical forms; milling rotates a cutter to remove material from secured work. Each creates waste and needs suitable machine settings, guarding and supervision. Accurate datums and measured checks matter more than a polished appearance alone.
- Casting — Casting pours a suitable molten material into a mould where it solidifies. Mould cavity, shrinkage, flow and safe handling affect the result. Sand casting can suit varied shapes; pressure die casting uses expensive reusable tooling suited to larger repeated runs.
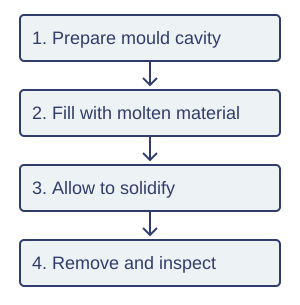
Casting sequence. Original schematic; apply the qualifications in the explanation. View full-size diagram - Sheet forming — Bending and pressing change sheet shape without necessarily removing material. Bend allowance, minimum bend radius and springback affect final dimensions. Work hardening or cracking can limit forming; prototype and test the material rather than assuming a sharp fold is always possible.
Springback is the material partly returning towards its earlier shape after the bending force is removed. Bend allowance accounts for the material length used around the curve of a bend.
- Joining — Mechanical fixings can allow disassembly. Brazing joins with a filler melted above 450°C while base metals remain solid; soldering uses lower-melting filler. Welding joins by coalescence, often melting base material. Appropriate methods depend on alloy, section, heat effects and supervised equipment.
Coalescence means that the materials unite at the joint. Welding can use heat, pressure or both, depending on the process; it is not always the addition of a lower-melting filler.
Quality and finishing
- Quality control — Measure dimensions, hole spacing, fit and defects against tolerances using a suitable rule, calliper or gauge. Check a drilled depth with calibrated stops and measurement. Casting porosity or a weak weld can be hidden; critical products need suitable tests, not visual approval alone.
Porosity means small holes or voids in the material. A casting can therefore look acceptable on the surface while containing internal defects.
- Corrosion protection — Galvanising coats steel with zinc, which provides barrier and sacrificial protection. Powder coating applies a powder then cures it; dip coating can cover a part with a protective polymer. Prepare and clean the surface first; damaged protection and environment influence durability.
Sacrificial protection means that the zinc corrodes in preference to the steel under the relevant conditions, helping protect it even where a small area is exposed.
- Anodising and polish — Anodising thickens aluminium's oxide layer through an electrolytic process, improving surface properties and allowing colour. Polishing smooths and brightens but does not provide the same protection as a coating. Choose a finish for appearance, wear and corrosion, with compatible preparation.
An electrolytic process uses an electric current in a suitable treatment liquid. In anodising, the controlled process builds up the metal’s protective oxide layer.
- Sustainable metal use — Durable replaceable components and separable alloys help repair and recycling. Scrap contamination can change alloy performance. Compare life-cycle impacts including energy, transport, use and recovery; a lightweight component may save use-phase energy but have high manufacturing impact.