Mr Kidman's Classroom


Revise the key ideas
Sources and selection
- Polymer production — Many polymers are made from petrochemical feedstocks. Crude oil is refined, fractions can be cracked to provide smaller molecules and monomers are chemically joined into polymers. Some feedstocks are renewable, but bio-based does not automatically mean biodegradable or suitable for home composting.
A feedstock is a starting raw material. Monomers are small molecules that can join into the much longer molecular chains of a polymer.
- Thermoplastic examples — Acrylic offers transparency and a polishable surface but can be brittle; HIPS is impact-modified for formed packaging. Polypropylene is light and useful for living hinges; polyethylene suits films or containers depending on grade. PVC can be rigid or flexible through formulation.
A living hinge is a thin flexible part moulded as part of the same component, allowing sections to bend relative to each other without a separate hinge.
- HDPE and PET — High-density polyethylene is a tough thermoplastic used in suitable containers and pipes. Polyethylene terephthalate is used for clear bottles and, in fibre form, polyester textiles. Processing grade and test evidence matter; identifying a polymer family does not establish food contact, reuse or temperature suitability by itself.
- Thermosetting examples — Epoxy bonds and encapsulates; melamine-formaldehyde provides a hard heat-resistant surface; phenol-formaldehyde suits heat-resistant electrical uses. Cross-linking prevents simple remelting after curing. Heat resistance has limits: no polymer should be described as unable to burn or degrade.
Cross-links connect neighbouring polymer chains. Curing is the process that develops the set, hardened material; heating it again does not simply reverse those links into a reusable melt.
- Polyester and urea resins — Cured polyester resin forms a thermoset matrix in suitable reinforced products; it differs from thermoplastic PET despite the shared word polyester. Urea-formaldehyde is used in suitable adhesives and moulded applications. Match resin, cure and safety controls carefully; emissions and chemical handling need approved procedures.
The matrix is the surrounding material that holds the reinforcement, such as fibres, in place and helps transfer forces between them.
- Additives — Pigments add colour; plasticisers increase flexibility in suitable polymers; UV stabilisers slow sunlight degradation. Fillers or reinforcements change properties and cost. Evaluate migration, durability, material compatibility and recycling rather than assuming an additive only has benefits.
Migration means a substance moving out of or through the material, for example an additive transferring into something that touches the product.
- Seating and fittings — Polymer seating needs adequate stiffness, toughness, stability and resistance to weather or cleaning. Electrical fittings need suitable insulation and temperature/fire performance. Match the grade to tested requirements; a recycled polymer of unknown composition is not automatically safe for these uses.
Stock and shaping
- Stock forms — Polymers come as sheets, rods, films, foam, powder and granules. Thickness or gauge, size and grade affect processing. Standard hinges and fasteners must distribute loads without splitting or excessive creep; include machining, shrinkage and trimming allowances when estimating quantities.
Creep is gradual deformation while a material remains under a load. A part may slowly change shape even though the load has not increased.
- Cutting and drilling — Select tools/settings for the polymer to reduce melting, chipping or cracking. Secure work, support the exit side of a drilled hole where appropriate and avoid overtightening fasteners. Laser cutting requires verified material compatibility: PVC must not be laser cut because hazardous corrosive gases can be produced.
- Vacuum forming — A suitable thermoplastic sheet is clamped, heated and drawn around a former by a pressure difference when air is removed. Cool before release and trim. Draft angles and appropriate vents aid release and detail; undercuts can trap the former and thickness varies during stretching.
Draft is a slight taper that helps a formed part release. Vents let trapped air leave; an undercut is an overhanging shape that can lock the former inside the cooled part.
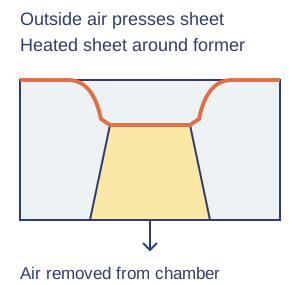
Vacuum forming cross-section. Original schematic; apply the qualifications in the explanation. View full-size diagram - Injection moulding — Granules are heated, forced into a closed mould, cooled and ejected. Complex repeated parts justify expensive tooling at high volume. Mould design must account for shrinkage, flow and release; setup cost makes it less suitable for a single simple classroom prototype.
- Extrusion and blow moulding — Extrusion pushes softened polymer through a die for a continuous section such as pipe. Blow moulding inflates a hot polymer form inside a mould to make hollow objects. Neither should be confused with cutting a shape from sheet; tooling and cooling affect quality.
- Drape forming and bending — A heated sheet can drape over a former; line bending heats a controlled strip before forming an angle. Temperature, bend radius and support affect appearance and accuracy. Use approved heating equipment and ventilation; do not attempt arbitrary heating of an unidentified polymer.
- Casting, printing and joining — Suitable resins can be cast and cured; 3D printing adds material layer by layer from a digital model. Adhesive bonding, solvent welding and heat welding depend on polymer compatibility. Printed layers may give directional strength and need supports; compare function and finish after testing.
Finish and environmental impact
- Quality and finishing — Check dimensions, warping, sink marks and function against the drawing. Polishing smooths suitable surfaces, printing adds information and vinyl decals add graphics. Use compatible preparation and coatings; laser settings influence cut dimensions but do not replace measurement or material safety checks.
Sink marks are shallow depressions in the moulded surface, often associated with uneven shrinkage as thicker regions cool.
- End of life — Identify polymers for sorting, minimise incompatible bonded layers and allow repair/disassembly. Thermoplastics can often be reprocessed with appropriate sorting; contamination and degradation limit quality. Thermosets cannot simply remelt, though other recovery routes exist. Recycling is not the same as harmless litter disposal.